For fast, high-volume internal threads in standard materials, tapping is your default. For deep holes, thin walls, exotic alloys, or expensive parts where a broken tool means a scrapped workpiece, thread milling is the safer, more flexible choice. Kennametal's threading guide puts the speed gap plainly: a 1/4"-20 tap runs a few seconds per hole; thread milling the same feature takes somewhat longer. That gap is real, and it matters at volume. But cycle time is only one variable.
Choose tapping when:
- You're running high-volume standard internal threads in aluminum, mild steel, or cast iron
- Thread size is 3/4" or smaller and the hole is through or shallowly blind
- Setup simplicity and machine cycle time are the dominant constraints
Choose thread milling when:
- Thread depth exceeds roughly 3× the nominal diameter
- Material is titanium, Inconel, hardened steel, or another difficult alloy
- Part value is high enough that a broken tap would cause a scrap event
Pro Tip: Before committing to either method, run your pilot diameter through a thread drill calculator to confirm minor diameter clearance. A wrong pilot hole is the most common reason taps break on the first pass.
Key Takeaways
Tapping wins on cycle time for standard internal threads in common materials; thread milling wins on flexibility, safety, and material range when the job demands it.
| Point | Details |
|---|---|
| Default to tapping for volume | High-volume standard threads in aluminum or mild steel: tapping is faster and cheaper per hole. |
| Thread mill for risk and depth | Threads deeper than 3× diameter, exotic alloys, or expensive parts favor thread milling's recoverable failure mode. |
| Pilot hole accuracy is non-negotiable | Wrong minor diameter is the leading cause of tap breakage; use a thread drill calculator before every job. |
| One thread mill covers multiple diameters | A single thread mill handles multiple diameters at the same pitch, reducing tool inventory versus size-specific taps. |
| Availzyemachinistpro connects decision to execution | The thread drill calculator, feeds & speeds, and G-code generator move you from method choice to running code in one platform. |
Table of Contents
- What tapping actually does and when it breaks down
- What thread milling actually does and why it needs a CNC
- How the cutting mechanics differ between the two methods
- Tapping vs thread milling: side-by-side comparison
- How to decide which method fits your specific job
- Practical setup: pilot holes, speeds, feeds, and inspection
- Using calculators to remove guesswork from the decision
- The trade-off most shops get wrong
- Availzyemachinistpro cuts setup time from decision to first cut
- Sources
What tapping actually does and when it breaks down
A tap is a single-pass thread cutter. It enters the pilot hole axially, and its cutting edges form a complete thread profile in one motion. Feed rate must match thread pitch exactly — one revolution equals one pitch advance — which is why rigid tapping (synchronized spindle and Z-axis) is the standard on modern CNC machining centers.
The main tap types each solve a specific problem:
- Spiral-point (gun) taps: Push chips forward ahead of the tap. Best for through holes in most materials. Fast and reliable.
- Spiral-flute taps: Pull chips back up and out of the hole. The right call for blind holes, especially in ductile materials like aluminum or stainless.
- Straight-flute (cut) taps: Minimal chip evacuation. Suited for brittle materials like cast iron where chips break small.
- Form/roll taps: No cutting edges — they cold-form the thread by displacing material. Stronger thread, no chips, but require a slightly larger pilot hole and don't work in brittle materials.
- Bottom taps: Short chamfer lead for threading close to the bottom of a blind hole. Usually used as a finishing tap after a plug tap.
Machine requirements matter here. Rigid tapping with a synchronized spindle is the standard for production work. Tension-compression (floating) holders give a small amount of axial float to compensate for minor feed errors, which is useful on older machines without true rigid tapping. MSCDirect's tapping guide notes that matching holder type and tap geometry to the hole type and material is one of the most reliable ways to cut tap breakage.
What thread milling actually does and why it needs a CNC
Thread milling removes material with a rotating cutter following a circular or helical toolpath programmed into the CNC. The cutter orbits the thread centerline while advancing axially one pitch per revolution. Xometry's comparison describes it well: thread milling can produce both internal and external threads, while tapping is limited to internal.
The main cutter types:
- Full-profile thread mills: Cut the complete thread form in a single helical pass. Faster than single-plane options and the most common choice for production thread milling.
- Single-plane (layered) thread mills: Cut one thread groove at a time, requiring multiple helical passes. Slower, but useful for very fine pitches or unusual thread forms. Kennametal's data confirms that single-plane mills generally take longer than full-profile due to the additional passes required.
- Combination drill/thread mills: Drill and thread in one tool. Useful for small-batch work where tool changes are expensive.
Thread milling requires a CNC with helical interpolation — simultaneous X, Y, and Z motion. That rules out manual mills and simple 2-axis machines. Spindle speeds are typically higher than tapping, and carbide is the standard material for thread mills. One significant advantage: Datron's threading comparison points out that a single thread mill can cover multiple diameters for the same pitch, cutting tool inventory compared to tapping, where each thread size demands its own tap.
How the cutting mechanics differ between the two methods
Tapping engages the full thread profile simultaneously across all cutting flutes. Every tooth is cutting at once, which generates high peak torque. For large-diameter taps — commonly noted around 3/4" and above — that torque demand can exceed what a standard machining center spindle handles comfortably without a geared head or high-torque spindle. Chip evacuation is also concentrated: all chips must exit through the flutes in a single axial direction, which creates problems in deep blind holes with ductile materials.
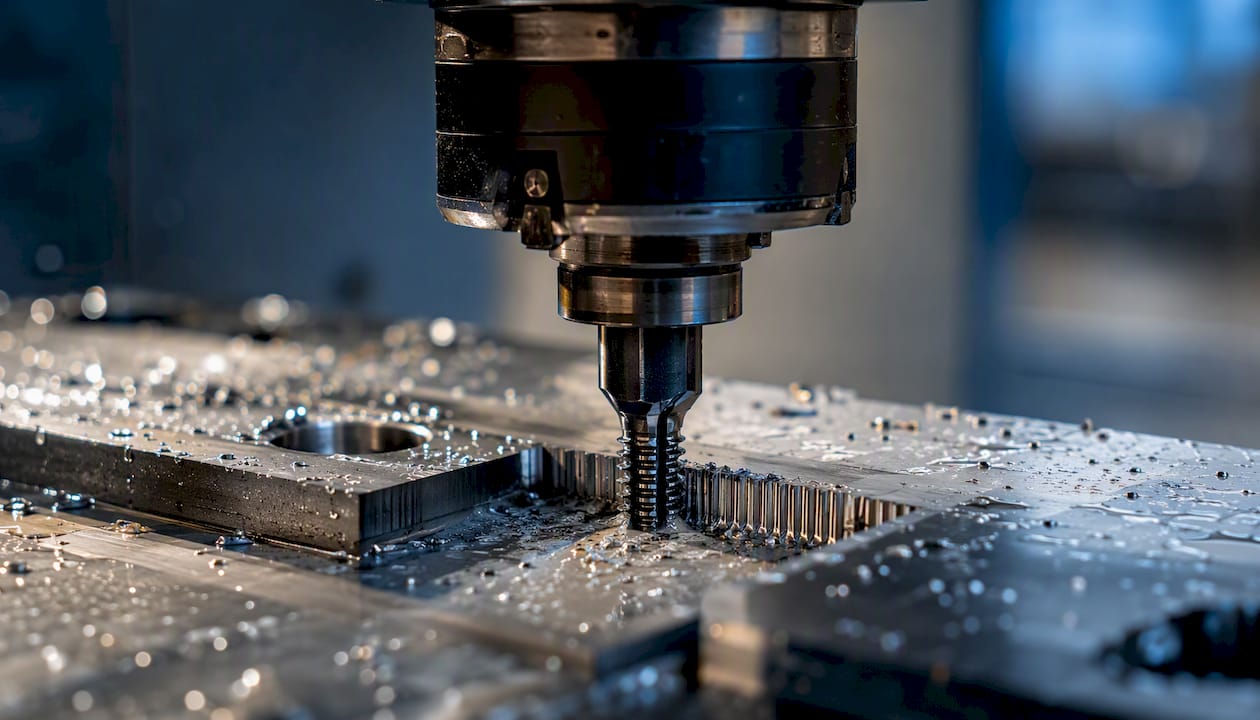
Thread milling distributes the cutting load radially in small incremental arcs. Peak cutting force at any moment is a fraction of what a tap generates. That lower force profile is why thread milling handles thin-walled parts without distortion and why it works in hard materials where a tap would simply snap.
Failure modes are fundamentally different. A broken tap in a blind hole is often unrecoverable without EDM or a tap extractor, and either outcome risks scrapping the part. A thread mill that breaks or deflects leaves the hole intact. You can re-enter, adjust the CNC offset, and finish the thread. MSCDirect's analysis frames this directly: taps are typically HSS and more prone to breakage; carbide thread mills are more predictable and the failure mode is far less catastrophic.
Pro Tip: Watch the spindle load meter during tapping. A sudden spike followed by a drop often means the tap has broken rather than completed the thread. On thread milling, a gradual load increase over successive holes usually signals tool wear — you still have time to change the cutter before a failure.
Tapping vs thread milling: side-by-side comparison
The table below covers the dimensions that matter most when you're making the call on the shop floor.
| Dimension | Tapping | Thread Milling |
|---|---|---|
| Speed / cycle time | Fast: a few seconds per hole (1/4"-20 benchmark) | Slower: somewhat longer per hole (same benchmark) |
| Tool cost | Low (HSS taps from a few dollars each) | Higher (carbide mills, $30 or more) |
| Per-hole cost at volume | Very low when tap life is good | Higher per hole, but lower scrap risk |
| Thread size range | One tap per size/pitch combination | One mill covers multiple diameters at same pitch |
| Blind hole suitability | Requires correct tap geometry; breakage risk | Excellent; no axial force at bottom of hole |
| Through hole suitability | Excellent | Good |
| Thread quality / accuracy | Good; limited adjustment after cutting | Excellent; CNC offset allows fit adjustment |
| Material suitability | Best in aluminum, mild steel, cast iron | Handles titanium, Inconel, hardened steels |
| Tool life | Shorter (HSS); breakage risk in hard materials | Longer (carbide); predictable wear |
| Machine requirements | Rigid tapping or floating holder; most VMCs | Helical interpolation; CNC required |
| Setup complexity | Low; standard G84 tapping cycle | Moderate; requires helical toolpath programming |
For a high-volume 1/4"-20 run in 6061 aluminum, tapping wins on every economic metric. The cycle time advantage compounds across hundreds of holes, and tap life in aluminum is long. For a low-volume Inconel deep-thread job — say, M10 at 35mm depth — thread milling is the only practical option. The torque required to tap that thread in Inconel is extreme, and a broken tap in a $500 Inconel billet is a hard conversation.
Uneed's CNC threading guide frames the decision the same way: tapping wins when cycle time and simple setup dominate; thread milling wins when risk, material, or depth make tapping impractical.
How to decide which method fits your specific job
Work through these questions in order. The first "yes" that applies usually determines your method.
- Is thread depth greater than 3× the nominal diameter? If yes, thread mill. Chip evacuation and torque in deep tapped holes are the leading causes of tap breakage.
- Is the material titanium, Inconel, hardened steel (>45 HRC), or another difficult alloy? Thread mill. Tap life in these materials is short and breakage risk is high.
- Is the part expensive enough that a broken tap would cause a scrap event? Thread mill. The recoverable failure mode alone justifies the slower cycle time.
- Is the hole blind with a tight depth tolerance? Thread mill gives you control over thread depth without axial force at the bottom.
- Do you need to cut the same pitch in multiple diameters? Thread mill. One cutter handles the range.
- Is volume high, thread size standard (1/4"-20 through 3/4"-10), and material aluminum or mild steel? Tap. The cycle time advantage at volume is significant.
- Does your machine lack helical interpolation? Tap. Thread milling requires true 3-axis simultaneous motion.
Scenario A — High-volume aluminum fixture plate: 200 holes, 1/4"-20, 0.5" deep, 6061 aluminum. Tap with a spiral-point tap in a rigid tapping cycle. Cycle time advantage is decisive; breakage risk in aluminum is low.
Scenario B — Low-volume titanium aerospace bracket: 8 holes, M8×1.25, 28mm deep, Grade 5 titanium. Thread mill with a carbide full-profile mill, through-tool coolant, and conservative feeds. A broken tap here is a scrapped part.
Practical Machinist's community experience confirms this pattern: shops default to tapping for quick standard threads and switch to thread milling when risk or material makes tapping impractical.
Practical setup: pilot holes, speeds, feeds, and inspection
Pilot hole and chamfer
The pilot hole diameter for tapping is critical. Too small and torque spikes; too large and thread engagement drops below the minimum for the application. A thread drill calculator gives you the correct minor diameter instantly — don't rely on memory or a worn-out chart.
Thread milling uses a larger pilot hole than tapping for the same thread, since the cutter enters the bore and orbits outward. The pilot diameter needs to clear the cutter body plus a small amount of radial clearance.
Add a chamfer at the hole entry for both methods. A 90° chamfer at 1.1–1.2× the major thread diameter breaks the sharp edge, guides the tap or mill entry, and prevents thread crests from chipping at the surface.
Starting speeds and feeds by material
| Material | Tapping SFM (starting point) | Thread Milling SFM (starting point) |
|---|---|---|
| 6061 Aluminum | ~200 SFM | ~400 SFM |
| stainless steel | ~20 SFM | ~200 SFM |
| Grade 5 Titanium | ~15 SFM | ~80 SFM |
| annealed steel | ~30 SFM | ~150 SFM |
| Hardened Steel (>45 HRC) | Not recommended | ~50 SFM (carbide only) |
These are starting points. Use a feeds and speeds calculator to dial in the exact RPM and feed rate for your specific tool diameter and material. For tapping, peck cycles help clear chips in deep blind holes; for thread milling, a spring pass (re-running the toolpath at zero additional depth) cleans up any deflection in the final thread form.
Workholding and runout
For tapping, total indicator runout (TIR) under 0.001" at the tap shank is the target. Excessive runout causes uneven thread loading and accelerates breakage. Use a quality collet or hydraulic holder rather than a standard drill chuck.
Thread milling is more forgiving of runout, but TIR above 0.002" will show up as inconsistent thread pitch diameter. Shrink-fit or hydraulic holders give the best results.
Coolant
Flood coolant works well for tapping in most materials. Through-tool coolant is the better choice for thread milling in stainless, titanium, and hardened steels — it clears chips from the cutting zone more effectively and extends tool life.
Thread inspection
Go/no-go thread gauges are the standard shop-floor check. A go gauge should pass freely; a no-go gauge should not enter. For tighter tolerance threads, a thread ring gauge or pitch micrometer gives more resolution. If threads are consistently tight, check pilot hole diameter first — undersized pilots are the most common cause of tight threads after tapping.
Using calculators to remove guesswork from the decision
The right calculators turn the thread mill vs tap decision from a gut call into a documented, repeatable process. Here's how each tool fits:
- Thread drill calculator: Confirms pilot hole diameter for both tapping and thread milling before you touch the machine. Prevents the most common cause of tap breakage. Use the Availzyemachinistpro thread drill calculator to get the correct minor diameter for any standard thread.
- Feeds & speeds calculator: Converts material, tool diameter, and SFM targets into RPM and feed rate. Critical for thread milling where spindle speed varies with cutter diameter.
- Tool deflection calculator: Estimates cutter deflection under radial load. Relevant for thread milling in hard materials where a long, small-diameter mill can deflect enough to affect pitch diameter.
- Power and torque calculator: Flags whether your spindle can handle the torque demand for a given tap size and material. If the torque requirement exceeds your spindle's rated output, thread milling is the answer.
- G-code generator: Converts your chosen parameters into a CNC-ready helical interpolation cycle for thread milling or a G84 tapping cycle. Reduces programming errors on the first run.
Pro Tip: Log every tool's hole count in a Tool Crib system alongside the tool cost. After a few jobs, you'll have real per-hole cost data for both tapping and thread milling in your specific materials — which makes the economic side of the thread mill vs tap decision a calculation rather than a guess.
The trade-off most shops get wrong
The standard advice is "tap for speed, thread mill for difficult jobs." That's correct as far as it goes, but it misses the more interesting question: what's the actual cost of a tap breakage event in your shop?
Most shops undercount it. The direct cost is the tap and the part. The real cost includes the machine downtime while someone attempts extraction, the EDM time if extraction fails, the rescheduling impact on the job behind it, and the conversation with the customer if the part ships late. On a $15 aluminum part, that math still favors tapping. On a $400 titanium component, it often doesn't — even if the thread milling cycle is twice as long.
Practical Machinist's community data reinforces this: experienced shops choose thread milling to reduce risk on expensive parts, and real-world constraints like tooling inventory and CAM skill determine the final choice more than theoretical speed comparisons. The shops that get this right aren't running thread milling everywhere — they've done the math on where the breakage risk actually lives in their job mix and protected those specific operations.
The other underrated factor is thread fit adjustment. A tapped thread is what it is. A thread milled thread can be opened or tightened by adjusting the CNC offset without changing the tool. For prototype work or first-article inspection, that flexibility is worth more than the cycle time difference.
Availzyemachinistpro cuts setup time from decision to first cut
Once you've picked your method, the gap between "I know what to do" and "the machine is running" is usually parameter selection and G-code. That's where shops lose time.
Availzyemachinistpro puts the thread drill calculator, feeds and speeds calculator, tool deflection check, and G-code generator in one platform. Pick your thread spec, confirm the pilot diameter, dial in the SFM for your material, check deflection on a long thread mill, and generate the helical interpolation cycle — without switching between five browser tabs or hunting for a chart. The Tool Crib logs tool life and per-hole cost automatically, so the economic side of the tap vs thread mill decision gets sharper with every job you run.

The Individual plan starts at $9.99/month with a 7-day free trial. Start with the thread drill calculator and run your next threading job with confirmed parameters instead of a best guess.
Sources
These are the primary references used throughout this guide, each worth bookmarking for deeper parameter selection or troubleshooting:
- Machining Guide: Thread Milling vs. Tapping - Kennametal
- Thread Milling vs. Tapping: What are the Differences? | Xometry
- Thread Milling vs. Tapping - Datron
- Thread milling vs tapping pros & cons - MSCDirect Knowledge Center
- Thread Milling vs. Tapping: What Works Best for You - Practical Machinist