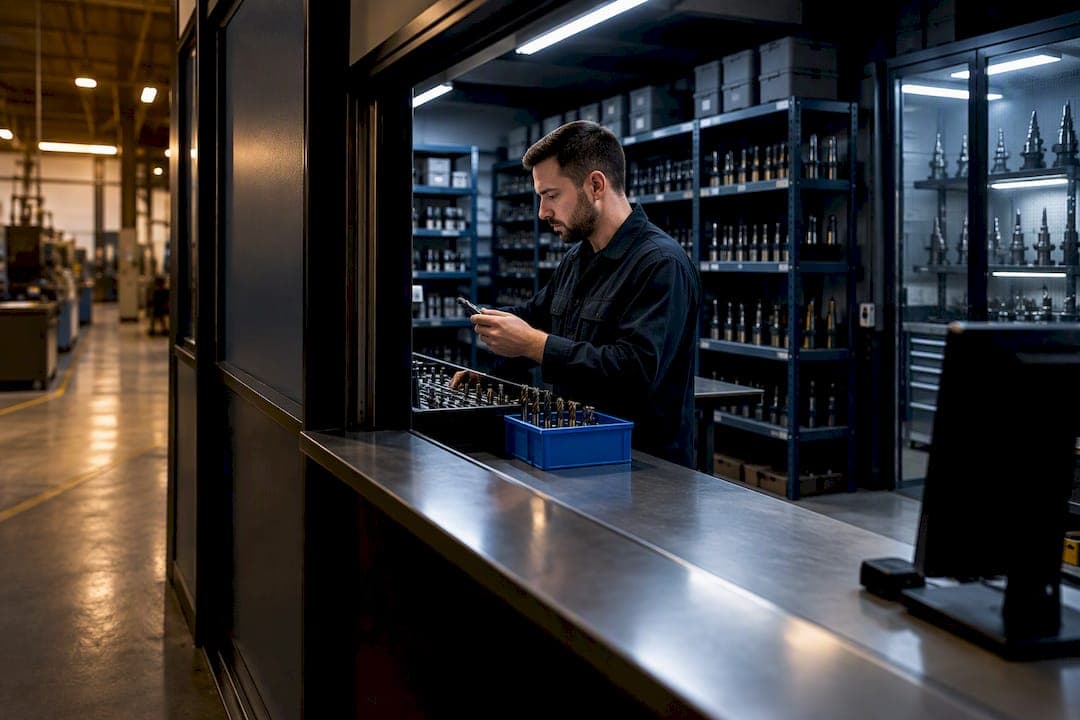
The best tool crib layout zones inventory by usage frequency and custody type, puts a staffed service window between the storage area and the floor, and keeps a dedicated staging station for prep work. Automate high-turn consumables first, keep returnable instruments in locker cells, and enforce strict location discipline before you touch any hardware. Get those three things right and everything else, from ergonomics to security, falls into place.
TL;DR:
- Proper layout places high-frequency items near the service window at waist height and separates bulky or rare tools on high or low shelves to minimize walk time.
- Automated high-turn consumables first, followed by job-linked tracking and returnable instrument management, before integrating with enterprise systems.
- Accurate records require unique IDs, location codes matching physical bins, and an enforced discipline to ensure staff trust and system reliability.
- Space planning must be proportional to SKU count, with a small crib for 200-500 SKUs at 100-200 square feet, and reserve capacity for future growth.
- Use shop-management software for ongoing discipline, tracking, and alerts, avoiding hardware dependency and maintaining organized, accessible inventory control.
Table of Contents
- Layout and zoning: arrange the crib for minimal walk time and clear custody
- Storage options and fixtures: choose cages, shelving, pegboard, drawers and locker cells correctly
- Inventory and tool records: minimum viable fields and why location discipline matters
- Ergonomics and workflow validation: test layout with real retrieval tasks
- Staging, teardown and pre-setup stations: a three-station workflow for CNC tooling
- Sizing and capacity planning: translate SKU counts to space and aisle requirements
- Security and access control: design roles, audit trails and custody for precision tooling
- Tracking systems and phased automation: what to automate, when, and what specs you need first
- Implementation checklist and phased rollout plan
- How integrated shop-management tools help operationalize these layout rules
- Maintenance and cleaning protocols for tool crib areas to ensure longevity and safety
- Emergency preparedness and safety procedures related to tool crib operations
- What most shops get wrong first
- A software option for keeping the discipline once it's built
- Sources
- FAQ
Layout and zoning: arrange the crib for minimal walk time and clear custody
The physical arrangement of a tool crib should mirror how often items move and who is accountable for them. Place the service window on the wall closest to the production floor, as every extra foot of walking adds up across dozens of daily retrievals. The attendant station sits directly behind that window, giving one person visual control of both the counter and the storage racks.
Fast-moving consumables belong at waist height within arm's reach of the window. Bulky or rarely used items go on high shelves or low pallet racks where an occasional climb or bend does not slow anyone down. Precision instruments and calibration-sensitive tools need their own enclosed zone, separate from bins holding disposable inserts or shop supplies.
According to Sortly's crib set-up guidance, the planning sequence starts with deciding which items actually belong in the crib, then measuring available capacity, choosing enclosure and storage types, and only then creating labeled zones. That order matters: labeling before you know your footprint just means relabeling twice.
A medium shop typically works well with three zones:
- Zone A, within 3 feet of the window: cutting tools, inserts, and daily consumables.
- Zone B, mid-depth shelving: fixtures, holders, and mid-frequency spare parts.
- Zone C, rear wall or high racks: bulk stock, seasonal items, and oversized fixtures.
Each zone should carry a printed code that matches the location code in your tool records, so an attendant or an app points a picker to the same physical spot every time.
Storage options and fixtures: choose cages, shelving, pegboard, drawers and locker cells correctly
Fixture choice should follow the item, not the other way around. Material Handling USA's crib enclosure guidance recommends wire-mesh security cages with Dutch door service windows for the perimeter, since mesh keeps visibility high while still controlling access. A Dutch door lets an attendant serve one person at the counter while keeping the rest of the storage area closed off.
Inside the cage, match the fixture to what it holds:
- Adjustable shelving with bin dividers for boxed SKUs and small parts that need clear counts.
- Pegboard or shadow boards for hand tools where a missing outline is the fastest possible inventory check.
- Drawer cabinets for precision instruments, gauges, and anything sensitive to dust or impact.
- Locker cells for high-value returnable tools that need individual check-out records.
Dimensions and weight decide dispensability more than anything else. An item too long, too heavy, or too irregular for a drawer or vending mechanism has to live on open shelving, no matter how often it turns over. Measure before you commit to a fixture type, not after.
Inventory and tool records: minimum viable fields and why location discipline matters
A tool crib is only as reliable as the records behind it. Reporting from Modern Machine Shop on machinist-owned tooling practices points to a minimum viable record that keeps a digital system trustworthy without demanding excessive data entry.
At minimum, each tool record needs:
- Unique tool ID and category.
- Critical geometry and any setup-relevant offsets.
- Vendor and part number for reordering.
- Physical location code that maps exactly to a drawer or bin.
- Expected usage or tool life, so wear gets tracked instead of guessed at.
Location discipline is the piece most shops skip, and it is the one that determines whether staff trust the system. A code like "7030-TC1-BIN14" works fine as long as the label on the drawer matches the code on the screen and everyone puts tools back in their labeled home. The exact syntax matters far less than the consistency of enforcement.
Before reorganizing or introducing any automation, clean out duplicate entries and obsolete SKUs. Migrating a messy item master into a new layout or a vending machine just moves the mess somewhere more expensive to fix.
Ergonomics and workflow validation: test layout with real retrieval tasks
A layout that looks efficient on paper can still create awkward postures once real tools and real bodies are involved. Ergonomics guidance for crib design recommends validating placement by watching people perform actual retrieval and handling tasks rather than trusting a floor plan alone.
A few rules hold up across most shops:
- Keep heavy items at waist height to avoid repetitive bending or overhead lifting.
- Put the highest-frequency items within 0 to 3 feet of the attendant or picker.
- Avoid layouts that force twisting motions when moving a tool from shelf to cart.
Run a short pilot before finalizing anything. Track picks for three days, gather feedback from whoever is doing the retrieving, and adjust shelf heights or aisle placement based on what actually slows people down.
Pro Tip: Time ten retrievals per station before and after a layout change. Ten samples is enough to see whether the new arrangement actually saves seconds, not just whether it looks tidier.
Staging, teardown and pre-setup stations: a three-station workflow for CNC tooling
CNC shops lose real setup time when teardown, sorting, and assembly all happen in the same cramped space near the machine. Contour Tool's crib design guidance describes a three-station workflow that pulls those tasks out of the machine area entirely.
- Teardown and inspection station: tools coming off a finished job get cleaned, inspected, and logged here, often using color-coded carts tied to a specific job or machine, with setup sheets attached for the next user.
- Sorting station: holders and assemblies get organized by retention system or by machine, so a picker grabs a complete set instead of hunting piece by piece.
- Pre-setup and assembly station: torque tools and gauges live here, along with a staged pool of tooling ready for the next job before it ever reaches the spindle.
This flow separates setup labor from machining labor, which reduces the time a machine sits idle while an operator hunts for a holder. It also enforces return-to-home behavior, since teardown always happens at Station 1 rather than wherever the last job ended.
Sizing and capacity planning: translate SKU counts to space and aisle requirements
Crib size should scale with SKU count and traffic, not with whatever spare corner happens to be available. Material Handling USA's sizing guidance puts a small crib holding 200 to 500 SKUs at roughly 100 to 200 square feet, while a medium crib holding 1,000 to 3,000 SKUs needs closer to 300 to 600 square feet.
Plan for these baseline needs regardless of size:
- Aisle clearance wide enough for a cart to pass without brushing shelving on both sides.
- Counter depth at the service window sufficient for setting down a full tool tray.
- Shelf linear footage calculated from your actual SKU list, not an estimate.
- Reserve capacity, roughly one extra bay per zone, for growth without a full rebuild.
Design the layout in modular sections from the start. Adding a bay of shelving or a second locker bank should not require moving anything already in place.
Security and access control: design roles, audit trails and custody for precision tooling
Access control should match risk, not slow down every transaction equally. Entitlement rules by role, shift, or department decide who can pull what, and those rules should map directly to whatever hardware controls the door or window, whether that is a keypad, a badge reader, or a simple sign-out sheet.
- A single Dutch door service window suits most shops with moderate traffic.
- High-traffic operations sometimes need multiple windows to avoid a line at shift change.
- Every transaction should capture employee, item, quantity, job ID, and time, since that data is what makes an audit trail useful later.
- Locker cells work best for high-value returnables and instruments that need calibration tracking, keeping custody clear even when several people share the same tool.
Tracking systems and phased automation: what to automate, when, and what specs you need first
Modernizing a crib is fundamentally an inventory and entitlement exercise, not a hardware purchase. According to KioskForce's tool crib modernization guide, the right sequence starts with a baseline and a clean item master covering pack size, dimensions, annual consumption, and entitlement before any dispensing equipment gets specified.
From there, migration typically follows four phases:
- Phase 1: automate the highest-turn, highest-cost consumables, since that is where measurable savings show up fastest.
- Phase 2: add job and entitlement capture, tying withdrawals to specific work orders.
- Phase 3: move returnable instruments into locker cells with individual check-out tracking.
- Phase 4: integrate the system with ERP or CMMS platforms for full visibility.
Not everything belongs in an automated system. Oversized items, one-off purchases, and anything that needs engineering judgment before issue should stay on open shelving under attendant control. Dimension and weight data from the cleaned item master determines whether a given part physically fits a vending mechanism, so verify fit with a planogram configurator before buying anything.
Implementation checklist and phased rollout plan
A reorganization goes smoother when it follows a fixed order rather than tackling layout, records, and automation all at once.
- Baseline current costs: attendant search hours, shrinkage, stockouts, and any informal hoarding of tools by individual machinists.
- Clean the item master: remove duplicate entries and obsolete SKUs before anything gets relabeled or migrated.
- Map items to storage and label zones: make sure every physical location code matches what appears in the tool record.
- Pilot the layout and staging workflow: test ergonomics and retrieval times for a short period before committing.
- Begin phased automation: start with fast-moving consumables per the four-phase sequence above.
- Review KPIs at 30, 90, and 180 days: adjust par levels and shelf placement based on actual pick data rather than assumptions.
How integrated shop-management tools help operationalize these layout rules
The minimum tool-record fields described earlier, unique ID, location code, vendor number, and expected usage, map closely to what a shop-management platform like Availzye Machinist Pro tracks natively, including check-in and check-out logs, job-linked transactions, and low-stock alerts. A platform is one way to enforce location discipline and measure pick data over time, not the only way. Whichever system you choose, verify fit through a trial period, a field reference, or a live demo before committing.
Maintenance and cleaning protocols for tool crib areas to ensure longevity and safety
A crib that looks organized on day one degrades fast without a maintenance routine. Set a weekly schedule for wiping down shelving, checking for rust on cutting tools, and confirming that shadow board outlines still match what is actually stored in each spot.

Precision instruments need a tighter cycle. Gauges and calibration-sensitive tools should get inspected monthly for damage or drift, with any unit outside tolerance pulled and flagged rather than returned to stock. Cutting tools and inserts benefit from a simple visual check at each restock: chipped edges or worn coatings get set aside for regrind or disposal instead of sitting in a bin where someone grabs them by mistake.
Floors and aisles need regular sweeping, since metal chips and oil residue near a tool crib create slip hazards on top of contaminating stored tools. Wire-mesh cages and Dutch doors should get checked periodically for loose hardware or damaged latches, since a compromised service window undermines the custody controls the whole layout depends on.
Build cleaning into the same cadence as your inventory counts. If an attendant is already walking the shelves for a cycle count, a five-minute visual sweep for damage, dust, or misplaced items costs almost nothing extra and catches problems before they become safety issues or lost-tool write-offs.
Emergency preparedness and safety procedures related to tool crib operations
A tool crib holding cutting oils, aerosol lubricants, or flammable cleaning solvents needs the same fire safety attention as any other storage area with combustible materials. Keep a rated fire extinguisher mounted near the service window, confirm it gets inspected on the same schedule as the rest of the shop, and make sure the crib layout does not block a clear path to the nearest exit.
Spill containment matters most around any zone storing cutting fluids or lubricants. Keep absorbent pads or spill kits within reach of that zone, not stored across the shop, and train attendants on where the nearest eye wash station or first aid kit is located relative to the crib.
Emergency shutoff points, whether for electrical equipment inside the crib or for compressed air lines feeding pneumatic tools, should be clearly marked and never obstructed by shelving or carts. If the crib includes any powered equipment, such as a bench grinder for tool sharpening, treat it as its own hazard zone with posted procedures.
Finally, include the crib in whatever evacuation plan covers the rest of the facility. An attendant working alone behind a Dutch door needs a clear, unobstructed path out, and that path should be walked and confirmed as part of any periodic safety drill rather than assumed to be fine because it looked fine during construction.

What most shops get wrong first
The most common mistake is automating a messy item master, which just moves confusion into an expensive machine. Poor label discipline and ignored ergonomics come next, usually because teams jump to hardware before fixing the basics. Start with shadow boards, labels that match the system exactly, and a real staging area, then track pick time, stockouts, attendant search hours, and shrinkage to see what actually improved.
— Availzye
A software option for keeping the discipline once it's built
Getting the layout, records, and location codes right is the hard part. Keeping them right over months of daily transactions is where most shops slip back into spreadsheets and paper logs. A shop-management platform's tool crib feature hosts tool records, check-in and check-out history, and low-stock alerts in one cloud-synced system with role-based access, so the discipline built into your layout does not depend on one person remembering the rules.
If you want to see how tool records, job-linked transactions, and alerts work together, you can explore the plans and try Availzye Machinist Pro with a 7-day free trial.
Sources
- Sortly — Tool crib set-up and inventory management guidance
- KioskForce — Tool crib modernisation guide
- Modern Machine Shop — When machinists own the tools
- Contour Tool — Tool crib design 101
- Material Handling USA — Tool crib enclosures and layout best practices
FAQ
What is the best layout for a small tool crib?
A small crib works best zoned by frequency: fast-movers at waist height near the service window, bulky or rare items on higher or lower shelves. Keep aisles clear enough for a cart and label every bin to match your tool record location codes exactly.
How do I decide what to automate first in a tool crib?
Start with the highest-turn, highest-cost consumables, since that is where KioskForce's guidance shows measurable savings appear fastest. Returnable instruments and full ERP integration come later, after job capture is in place.
What information does a tool record need at minimum?
A workable tool record needs a unique tool ID, category, critical geometry, vendor part number, physical location code, and expected tool life. Modern Machine Shop's reporting emphasizes that location discipline, matching the code on screen to the label on the drawer, is what makes staff trust the system.
How much space does a tool crib need?
Space scales with SKU count: Material Handling USA puts a small crib of 200 to 500 SKUs at roughly 100 to 200 square feet, and a medium crib of 1,000 to 3,000 SKUs at 300 to 600 square feet. Add reserve capacity for growth so you avoid a full rebuild later.
Can software help manage a tool crib without buying vending hardware?
Yes, a shop-management platform can host tool records, check-in and check-out logs, and low-stock alerts without any dispensing hardware. Availzye Machinist Pro's Tool Crib feature works this way, giving attendants a digital system to enforce location discipline before any automation investment.