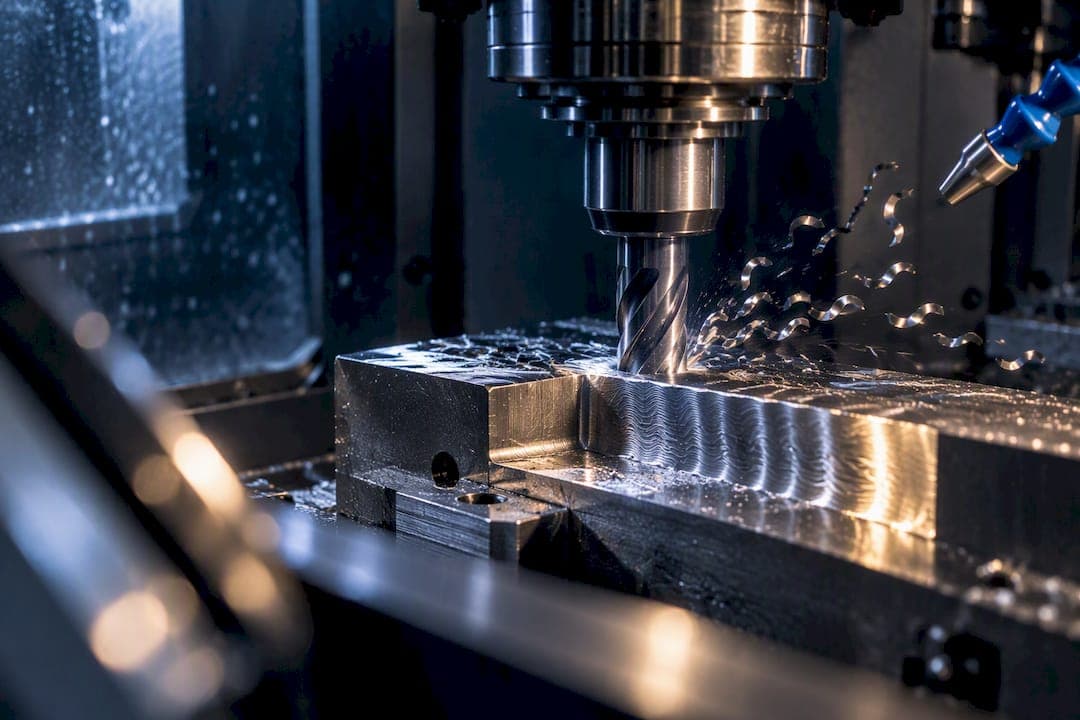
Shorten the tool's stick-out or swap to a rigid holder, drop your axial depth of cut, and nudge spindle speed into a nearby stable zone. Those three moves resolve most chatter within a few minutes on the machine. Confirm the fix with a short test cut and a quick listen or a measurement pass, ideally cross-checked against a stability lobe diagram. Tools like Availzye Machinist Pro can speed up that verification by predicting stable speed and depth combinations before you cut metal.
TL;DR:
- Reducing axial depth of cut by 20-30 percent and shortening tool overhang can quickly eliminate chatter in most milling scenarios.
- Shifting spindle speed by a moderate step or changing milling direction can move the operating point into a stable lobe without redesigning tooling.
- Confirming chatter frequency with FFT analysis and recording parameters helps build a reliable shop-specific stability map for future reference.
- Ensuring machine and toolholder integrity, including checking for looseness and wear, is crucial before adjusting cutting parameters to prevent chatter.
- Using process damping features like wiper flats or fixture redesign can be necessary for delicate parts or long-reach setups when parameter tweaks alone fail.
Table of Contents
- Quick shop-floor checklist: stop chatter in minutes
- Diagnose: how to tell chatter from other problems and measure its frequency
- Why chatter happens: regenerative chatter, stability lobe diagrams, and the energy balance
- Adjust cutting parameters: speed, feed, depth, immersion, and spindle-speed modulation
- Tooling and workholding: holders, overhang, cutter geometry, and process damping
- When to increase damping or stiffness: passive vs. active countermeasures
- Shop maintenance and machine checks that prevent chatter
- Practical workflow: measure → adjust → verify (repeatable steps to kill chatter)
- Perspective: an Availzye machinist's view, engineering the fix, not guessing
- How Availzye Machinist Pro helps diagnose and prevent chatter
- Sources
- FAQ
Quick shop-floor checklist: stop chatter in minutes
Chatter rarely needs a redesign. It needs a sequence, run in order, with attention paid to what changes and what doesn't.
- Stop or slow down immediately if the tool, holder, or part looks at risk of damage from the vibration.
- Cut axial depth of cut by 20 to 30 percent and see if the marks and sound clean up.
- Shorten the tool's stick-out or move to a stiffer holder if depth reduction alone doesn't fix it.
- Shift spindle speed up or down by a moderate step rather than a small nudge, since chatter often lives in narrow speed bands.
- Increase feed per tooth slightly once the cut sounds stable, since a heavier chip load can raise the chatter threshold in some setups.
Watch the part and the sound as you go. A cut that quiets down and stays quiet through a full pass is a good sign. One that clears up for a second and then returns usually means you're still near an unstable lobe and need a bigger speed change or a stiffness fix.
If the chatter reappears after re-fixturing or a tool change, stop guessing and start recording. Note the RPM, feed, depth of cut, holder type, and tool length for every attempt, successful or not. That log becomes the raw material for a shop-specific stability lobe map later.
Pro Tip: Write down the exact parameters the moment a cut goes quiet, not after the job is done. Memory is unreliable, and that data point is worth more than the finished part.
Diagnose: how to tell chatter from other problems and measure its frequency
Chatter marks have a signature that separates them from tool wear, deflection, or a bad insert.
- Repeating waviness: chatter leaves a regular, rippled pattern on the surface, unlike the smeared or torn look of a dull edge or the localized gouge of a broken tooth.
- Tonal sound: a chatter event produces a distinct pitch, often noticeably different from the steady tooth-pass whine of a clean cut.
- Frequency mismatch: if the dominant sound doesn't line up with the tooth-pass frequency (spindle RPM times number of teeth, divided by 60), you're likely hearing structural chatter tied to a natural frequency in the machine, tool, or workpiece rather than a forced vibration.
- Load signature: a spindle-load monitor or accelerometer will show a spike at a frequency that doesn't match any expected forcing frequency, which is the clearest confirmation.
A microphone or accelerometer paired with an FFT analysis will show that dominant frequency directly. Milling-sound mapping with a microphone and FFT can identify chatter frequencies without a full dynamic model, which makes it a practical shop-floor method rather than a lab-only technique. Once you know the chatter frequency, you can calculate spindle speeds that shift the tooth-pass rate away from that frequency, which is the basic logic behind moving between stability lobes. Guidance on capturing that signal in real time is covered in more detail in spindle-load monitoring practices built around the 1 to 2.5 kHz range common in milling.
Why chatter happens: regenerative chatter, stability lobe diagrams, and the energy balance
Regenerative chatter starts small. A tooth passing over a slightly wavy surface, left by the previous pass or the previous tooth, encounters a varying chip thickness. That variation creates a fluctuating cutting force, which excites vibration in the tool, spindle, or workpiece. The vibration leaves its own waviness behind, and the next pass amplifies it. Regenerative chatter is a self-excited, deterministic vibration driven by surface waviness left over from a prior cut, according to research on sound mapping for stability lobe identification, and the effect compounds unless something interrupts it.
Stability lobe diagrams chart this behavior directly. They plot spindle speed against axial depth of cut and mark out which combinations are stable and which will chatter. The stable regions form lobes, and the boundaries between them are not smooth. A small shift in RPM, sometimes just a few hundred rotations per minute, can move you from an unstable zone into a stable pocket at the same depth of cut. That's why "just try a different speed" works as often as it does: you're not fixing the underlying physics, you're sidestepping it.
Underneath the diagram is an energy balance. Cutting forces feed energy into a vibration mode at its natural frequency. Damping, whether from the structure, the joints, the tool, or the material, removes energy. Chatter grows when the energy going in from cutting exceeds what the system can dissipate. Anything that adds stiffness or damping shifts that balance in your favor, which is why a shorter tool or a stiffer holder can stop chatter even without touching speed or feed. Parameter changes buy you a stable window inside the current setup. Structural changes, shortening overhang, upgrading a holder, adding a damper, expand how much stable window exists in the first place.

Adjust cutting parameters: speed, feed, depth, immersion, and spindle-speed modulation
Once you've confirmed chatter, the fastest lever is usually spindle speed, but the size of the step matters more than the direction.
- Change speed in meaningful steps, not tiny nudges. Moving 5 to 15 percent up or down tends to cross lobe boundaries; a 1 to 2 percent tweak often lands you in the same lobe you started in.
- Reduce axial depth of cut first when you're not sure which lever to pull. It's the fastest change to test and often the one that matters most in the stability equation.
- Check immersion ratio and milling direction. Down-milling and up-milling shift where unstable lobes fall, and switching between them can move you out of a chatter zone without touching speed at all, a relationship confirmed by collocation-based stability analysis of up- and down-milling behavior.
- Raise feed per tooth cautiously. A heavier chip load can raise the chatter threshold in some cuts, but it also raises cutting forces and deflection, so it helps in light finishing passes more than in heavy roughing.
- Consider chip thinning at low radial engagement. At shallow cuts, the effective chip load is thinner than the programmed feed suggests, so what looks like a feed increase may not actually raise forces the way you expect.
Spindle-speed variation, cycling RPM slightly during the cut rather than holding one value, can disrupt the regeneration cycle in some jobs. It works best on long, continuous cuts where a fixed speed sits right on an unstable boundary, but it adds programming complexity and isn't a first resort. Try the simpler speed, depth, and direction changes before reaching for SSV.
Tooling and workholding: holders, overhang, cutter geometry, and process damping
If parameter changes only partially fix the problem, the tool and holder are usually the next place to look, and often the highest-value one.
- Shorten stick-out before anything else. Stiffness falls off sharply, closer to a cubic relationship, as tool overhang increases, so trimming even a small amount of length off the exposed tool can produce an outsized gain in rigidity.
- Move to a rigid holder. Shrink-fit and hydraulic holders grip more of the tool shank and transmit less runout than a standard collet, and a worn or dirty taper undoes any holder upgrade regardless of type.
- Try variable-pitch or variable-helix cutters when speed and depth changes aren't enough. Uneven tooth spacing disrupts the regenerative cycle by changing the timing between successive cuts on the same surface, an approach detailed in chatter stability research on unified dynamic models and tool-design suppression methods. A closer look at variable-pitch and variable-helix cutter design is available in this high feed milling guide.
- Use process damping at low cutting speeds. Wiper flats and flank contact features increase friction damping at the tool-workpiece interface, which the same research identifies as especially effective in low-speed and interrupted cuts.
Pro Tip: Before buying a new holder, check whether your current one is even seated correctly. A clean taper with proper contact often outperforms an expensive upgrade on a dirty or worn one.
When to increase damping or stiffness: passive vs. active countermeasures
Not every chatter problem clears up with a tool change. Thin walls, long reach setups, and delicate fixtures sometimes need added damping.
- Passive dampers and tuned mass dampers are the low-cost, low-complexity option, but they only work well near the frequency they're tuned for, which limits their range across different jobs.
- Active and semi-active systems cover a wider frequency range and adapt to changing conditions, but they cost more and take more setup and expertise to run, a trade-off outlined in a review of chatter suppression strategies for thin-wall milling.
- Fixture redesign matters as much as the tool. Sacrificial supports under thin walls and revised clamping points can remove a vibration mode entirely instead of just damping it.
Try tooling and process changes first. Reach for dampers or fixture redesign only when the part geometry or production volume makes those constraints unavoidable.
Shop maintenance and machine checks that prevent chatter
A surprising share of chatter complaints trace back to maintenance, not programming.
- Check spindle taper and runout. A worn taper or a chipped collet seat introduces vibration no parameter change will fix.
- Inspect holder cleanliness and seating every time a new tool goes in, since debris on the taper face changes contact and stiffness.
- Verify machine leveling and mechanical looseness, including backlash, loose way covers, and worn bearings, since these lower the whole machine's effective stiffness. A tooling and machine accessory check list is a useful reference when setting up a routine inspection schedule.
- Confirm clamping torque and fixture stiffness on every setup, and add sacrificial supports for thin or overhanging sections.
- Log every chatter incident and its fix. RPM, depth, holder, and outcome, recorded over time, builds a practical stability map specific to your machines and tooling.
Practical workflow: measure → adjust → verify (repeatable steps to kill chatter)
A repeatable process beats trial and error, especially across a shop with more than one operator.
- Capture evidence first. Take a photo of the marks, record audio or run an FFT, and note the spindle load at the moment chatter appears.
- Apply fixes in order of expected impact. Shorten stick-out, reduce depth of cut, then change spindle speed, testing each change before stacking the next.
- Re-measure after each change. Check the surface finish and listen for the tonal sound to confirm it's actually gone, not just quieter for a moment.
- Escalate when the basics don't hold. If tooling and parameter changes fail, move to re-fixturing, variable-pitch cutters, or a damping solution, and bring in engineering support for parts where thin walls or tight tolerances leave little room for error.
Perspective: an Availzye machinist's view, engineering the fix, not guessing
Most chatter fixes on a shop floor come from habit, not measurement. That works until it doesn't. Measuring the actual chatter frequency and writing down what worked turns a lucky speed change into a repeatable process the next operator can use.
The most common mistake is skipping the machine check and blaming the tool. A worn taper or loose gib will chatter no matter how good the cutter is. Maintenance first, tooling second, speed changes third, usually in that order of return. Availzye Machinist Pro fits into that habit by making chatter prediction and parameter selection something you check, not something you remember.
— Availzye
How Availzye Machinist Pro helps diagnose and prevent chatter
Instead of switching between a chatter calculator, a feeds and speeds spreadsheet, and a paper logbook, Availzye Machinist Pro keeps the Chatter Prediction, Feeds & Speeds, and Tool Deflection calculators in one place, alongside a Job Tracker for recording what actually worked. Run a quick prediction before you cut, log the RPM and depth that cleared the chatter, and the next job on that machine starts from data instead of memory. Plans run from Individual at 9.99 CAD per month up through Team at 49.99 CAD per month, all with a 7-day free trial, at Availzye-machinist-pro.
| Tool | What it helps with |
|---|---|
| Chatter Prediction | Estimates stable speed and depth combinations before cutting |
| Feeds & Speeds | Sets baseline parameters to avoid starting near an unstable zone |
| Tool Deflection | Flags excessive stick-out before it becomes a chatter problem |
| Job Tracker | Logs successful fixes for repeatable use across jobs |
Sources
Research on stability lobes, chatter mechanisms, and damping methods informed the technical claims above.
- Sound mapping for stability lobes diagram identification in milling processes
- Chatter Stability of Machining Operations
- A review of chatter suppression in thin-wall milling: strategies, mechanisms, and applications
FAQ
How to reduce chatter when milling?
Shorten the tool's overhang, reduce axial depth of cut, and shift spindle speed into a nearby stable zone, then confirm with a test cut. These three changes resolve most chatter cases without needing new tooling or fixtures.
What causes machining chatter?
Chatter is usually regenerative: a tooth cutting over surface waviness left by a previous pass creates a varying chip thickness that excites vibration, and that vibration leaves more waviness behind. Regenerative chatter is a self-excited, deterministic vibration according to sound mapping research for stability lobe identification, which grows until something interrupts the cycle.
What does CNC chatter sound like?
Chatter has a distinct tonal quality, often a higher-pitched squeal or a rattling buzz that doesn't match the steady tooth-pass whine of a clean cut. If the pitch doesn't line up with spindle RPM times tooth count, you're likely hearing a structural vibration tied to a natural frequency rather than normal cutting noise.
How to avoid chattering in turning?
The same core principles apply: reduce overhang on the tool and workpiece, check for looseness in the toolholder and tailstock, and adjust spindle speed to avoid the part's natural frequency. Immersion and depth of cut matter less directly in turning than in milling, but rigidity and speed selection still drive most fixes.