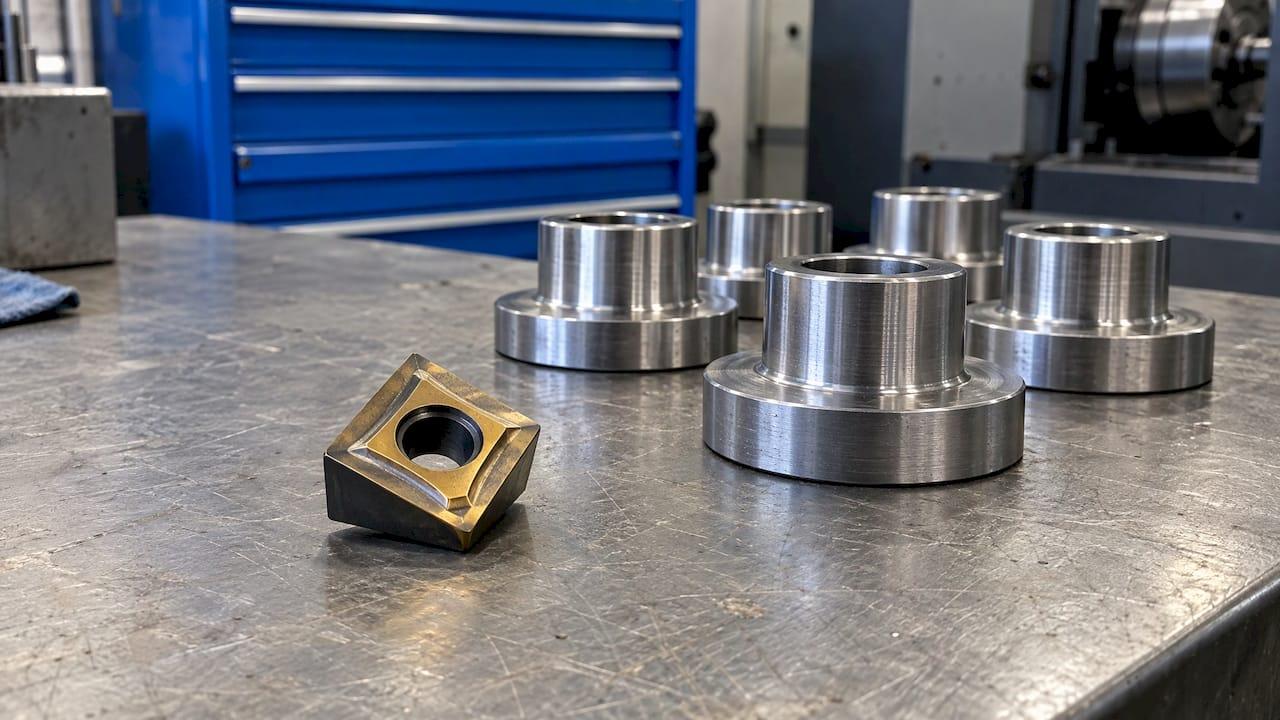
Tool cost per part is the price of a cutting edge divided by the number of parts that edge produces, plus the cost of the time you lose changing it. A $20 end mill that cuts 50 identical brackets costs $0.40 per part in tool price alone. Add tool-change labor, regrinds and scrap, and the true figure is usually higher, and it often points to a different tool than the cheapest one on the shelf.
This guide gives you the formulas, a worked example you can copy into a spreadsheet, and the inputs that most quotes leave out.
TL;DR
- Basic formula: tool price ÷ (usable edges × parts per edge). Count only edges you really use, not the number printed on the box.
- True tool cost adds tool-change time at your shop rate, divided by parts per edge, plus regrind cost for solid tools.
- Measure tool life on your own machines and materials. Catalog life is a starting point.
- A tool that costs more but cuts cycle time or lasts longer very often lowers total cost per part, because machine time usually outweighs tool spend.
- Convert tool life in minutes to parts: life in minutes ÷ cutting minutes per part.
Table of Contents
- The basic formula
- Add the costs the price tag hides
- When tool life is in minutes, not parts
- A worked example you can reuse
- Why machine time usually dominates
- Finding the cost-minimizing tool life
- What belongs in a quote and what does not
- How to measure your own numbers
- Breakage and the cost of failure
- Perspective
- Put your numbers to work
- FAQ
- Sources
The basic formula
Start with the simplest version. A tool's cost per part is the price of one cutting edge divided by the parts that edge produces. The same source points out that a tool at twice the price yielding 400 parts beats a cheaper one yielding 100, because the cost per part is half.
For an indexable insert:
Tool cost per part = insert price ÷ (usable edges × parts per edge)
For a solid tool, replace "usable edges" with the number of lives you will get, meaning the first life plus the regrinds you expect.
Two habits keep this number honest:
- Count usable edges. A square insert may say eight edges on the box. If your operation only lets you use four, divide by four.
- Use observed life. Log the actual parts per edge at the speed and feed you run, not the figure in the catalog.
Add the costs the price tag hides
The insert price is often the smallest piece of tooling cost. A fuller version looks like this:
True tool cost per part = (cost per edge + tool-change time × shop rate) ÷ parts per edge
For solid tools, add the regrind cost to the numerator. Where do the extra terms come from?
- Tool-change time. Every index or swap stops the spindle. Multiply minutes by your machine rate and spread it across the parts that edge made.
- Regrinds. A well-executed regrind typically costs 30 to 40% of a new tool and returns 85 to 95% of original performance, according to a regrinding specialist quoted in American Machinist. Use your own regrind invoice and your own measured performance after regrinding.
- Scrap. If tool wear causes bad parts, divide the operation cost by (1 − scrap rate) to get the cost of a good part.
- Slower feeds on worn tools. Operators who push a worn tool often back off the feed, which stretches cycle time. That cost lands in machining time, not in the tool line, so it is easy to miss.
When tool life is in minutes, not parts
Catalogs and tool-life tests usually give minutes of cutting. To convert, divide tool life in minutes by cutting minutes per part. A 15-minute edge life with 0.5 minutes of cutting per part gives 30 parts per edge.

The same relationship appears in academic form. A published machining cost model gives tooling cost per component as (machining time ÷ tool life) × (tool cost + tool-change time × labor rate). Read it this way: the fraction of a tool's life each part consumes, times the full cost of a tool life including the change.
If you want to see how speed changes tool life, the Taylor relationship (V × T^n = constant) is the standard tool. We walk through it in two worked examples of Taylor's tool life equation.
A worked example you can reuse
The numbers below are an illustration, not a measured result. Swap in your own.
Setup: a part with 6 minutes of cutting time, a shop rate of $90 per hour ($1.50 per minute), and a 2-minute index.
| Input | Standard insert | Premium insert |
|---|---|---|
| Insert price | $12.00 | $16.00 |
| Usable edges | 4 | 4 |
| Cost per edge | $3.00 | $4.00 |
| Parts per edge | 25 | 40 |
| Cutting time per part | 6.0 min | 5.4 min (10% faster) |
Standard insert, per part:
- Insert: $3.00 ÷ 25 = $0.12
- Index time: 2 min × $1.50 = $3.00, ÷ 25 = $0.12
- Machine time: 6 min × $1.50 = $9.00
- Total: $9.24
Premium insert, per part:
- Insert: $4.00 ÷ 40 = $0.10
- Index time: $3.00 ÷ 40 = $0.075
- Machine time: 5.4 min × $1.50 = $8.10
- Total: $8.275
The premium insert costs 33% more per piece yet saves about $0.97 per part. On a 2,000-part order that is roughly $1,930. Notice that the tool line barely moved, from $0.24 to $0.175 per part. The savings came almost entirely from machine time.
That pattern appears in published shop-floor examples too. A trade magazine case showed many shops would reject an insert that cost 33 percent more without testing it, even though the higher metal-removal rate and doubled parts per edge made it the cheaper option overall.

Why machine time usually dominates
Tooling is a modest fraction of total cost for most shops running most jobs, because the hourly machine rate (machine, floor space, power, operator, overhead) is so much larger than what you spend on cutters in the same hour. That is why the useful question is rarely "which tool is cheapest?" and more often "which tool gives the lowest cost per good part?"
The exceptions are harder materials and tight tolerances. One published breakdown puts tooling at typically 3 to 10% of a quote, reaching 10 to 20% on hard materials such as titanium. If you cut those materials, the tool line deserves closer tracking.
Finding the cost-minimizing tool life
Running faster saves cutting time but burns edges faster. Cost per part therefore has a minimum. Using Taylor's equation, the tool life for minimum cost is (1/n − 1) × (tool-change time + tool cost ÷ labor rate), where n is the Taylor exponent for your tool and material pair.
The practical reading:
- Expensive edges or slow tool changes push the best speed down, toward longer life.
- Expensive machine time pushes the best speed up, toward shorter life.
- The speed for maximum production rate is always higher than the speed for minimum cost.
That last point matters when you quote. Running at the fastest possible rate is not the same as running at the lowest cost per part.
What belongs in a quote and what does not
Tool cost per part is one line in a larger picture. A few definitions help you avoid double counting:
- Tool wear in the hourly rate. Some shops fold consumables into the machine rate, others bill them separately. One published comparison shows $15 of carbide inserts appearing as $85 per hour at one shop and $70 per hour plus $15 tooling at another. Pick one method and use it consistently.
- Standard tool list. A shop's standard tools are an indirect cost maintained regardless of customer mix, while tooling dedicated to a specific product is typically customer-owned.
- Fixtures. Jigs and fixtures are commonly shown as separate line items and can be a one-time nonrecurring expense, so keep them out of your per-part tool figure.
For the rest of the cost stack, see our machining cost breakdown and the guide to machining cost estimation for shops.
How to measure your own numbers
Formulas only work with real inputs. A simple routine:
- Log parts per edge. Record the count each time an edge is indexed or a tool is retired, by tool, material and job.
- Record why it ended. Wear, chipping, breakage and chatter lead to different fixes.
- Time the change. Stopwatch an index and a full tool swap, including re-touching off if needed.
- Set your machine rate. Include the machine, floor, power, operator and overhead, then use it for every machine-time and tool-change calculation.
- Recalculate when something shifts. A new coolant, a harder material lot or a feed change all move real tool life away from the catalog figure.
Workholding affects this too: rigidity and vibration influence how long edges last, which is why it is worth reading about advanced workholding for CNC when you are trying to estimate real-world tool life.
Feeds and speeds are the other big lever on edge life. Our guide to calculating feeds and speeds shows how to set starting parameters before you collect your own data.
Breakage and the cost of failure
An unplanned failure costs far more than the insert. In titanium aerospace work, one report puts the true cost of a cheap insert failing early at $800 to $1,200 once tool-change downtime and possible workpiece damage are counted. Your numbers will differ, but the method carries over to any job where a part is expensive.
To include breakage in your per-part figure, track the number of unplanned changes per 100 parts, then add (breakage rate × cost of one failure) to your per-part total. Cost of one failure is the tool, the lost machine time at your shop rate, and any scrap.
Perspective
We built Availzye Machinist Pro around one idea: a cost per part is only as good as the numbers feeding it, and those numbers live in too many places. Tool life is in someone's notebook, machine rate is in a spreadsheet, and the job's cycle time is in the CAM system.
When those inputs sit in separate places, shops fall back on the price tag of the insert, because it is the one number everyone can see. We think the better habit is to treat tool life, tool changes and cycle time as one calculation.
That is why our platform pairs engineering calculators, such as feeds and speeds, chip thinning and tool deflection, with a Tool Crib that supports tool life logging and a cost estimator. Our approach is designed to let a shop move from catalog numbers to its own measured numbers, in one cloud-synced place, without switching between apps and paper logs.
Availzye
Put your numbers to work
If you are ready to stop recalculating by hand, the Cost Estimator is built to bring machine time, tooling and job inputs together. Pair it with the Feeds & Speeds calculator to see how a speed change moves your cycle time, and log results in the Job Tracker.
Availzye Machinist Pro is offered in three plans: Individual at $9.99 CAD per month, Small Shop at $24.99 CAD per month and Team at $49.99 CAD per month, each with a 7-day free trial. You can see the plans on our site.
FAQ
How do you calculate tool cost per part?
Divide the cost of one cutting edge by the parts that edge produces. For a $12 insert with four usable edges making 25 parts per edge, that is $3.00 ÷ 25, or $0.12 per part. Then add tool-change time at your shop rate, divided by the same parts per edge, for the true figure.
What should I include besides the insert price?
Include tool-change or indexing time at your machine rate, regrind cost for solid tools, and scrap caused by wear. Count only the edges you actually use, and use observed tool life from your own machines and materials rather than the catalog figure.
Is a cheaper tool always cheaper per part?
No. Cost per part depends on tool life, cycle time and downtime together. A tool that costs more but lasts longer or cuts faster often lowers the total, as the worked example above shows, with a 33% pricier insert saving about $0.97 per part.
How do I convert tool life in minutes to parts per tool?
Divide tool life in minutes by the cutting minutes per part. A 15-minute life with 0.5 minutes of cutting per part gives 30 parts per edge. Use that parts-per-edge figure in the cost formula.
Sources
- Cost Per Part, Not Cost Per Tool
- Cutting Tool ROI Calculator
- Cost Modeling and Economic Analysis of Machining Processes
- Connected Regrinding Workflow Helps Combat Rising Carbide Costs
- Low cost vs. real cost
- CNC Machining Tooling Cost: How Cutters and Tool Wear Affect Price
- 6 Hidden Fees in CNC Turning Quotes Explained
- Job shop estimating: Programming, fixtures, and special handling
- Carbide insert grade selection for titanium milling